+
WACKER High-Performance Binders Help Reduce Carbon Footprint
Cement

WACKER High-Performance Binders Help Reduce Carbon Footprint

Manufacturers of dry-mix mortars – in particular tile adhesives – are currently facing the challenge of adapting their formulations, which are based on Portland cement (CEM I). Why? With the aim of reducing CO2 emissions, the cement industry is increasingly switching its production to Portland composite cements (CEM II). With a wide range of VINNAPAS® dispersible polymer powders that ensure high-performance formulations of dry-mix mortars, even with CEM II cements, WACKER helps dry-mix mortar manufacturers achieve this transition. At the 2025 European Coatings Show, which will be held in Nuremberg, Germany, from March 25 to 27, WACKER will be presenting a portfolio including polymer dispersions, dispersible polymer powders and solid resins – products that are used in numerous industries to enhance product properties.

The cement industry is responsible for around 8% of the world’s total CO2 emissions. Considered a particularly energy and emissions-intensive sector, the cement industry has taken various measures aimed at reducing its CO2 emissions for the benefit of the climate. Some of these measures involve changing the product portfolio to include cements with a lower proportion of Portland clinker. (Portland clinker is the heated part of the cement that is responsible for the setting and hardening of the cement when water is added.) This trend is likely to continue, especially as many industrialized nations have set themselves the goal of producing climate-neutral cement from 2050. In several European countries, among them the Czech Republic, manufacturers have already removed CEM I from their portfolio.

In terms of volume, cement, alongside sand, is the most important component of dry-mix mortars and, consequently, tile adhesives. It serves as a binding agent. CEM I is used in many commercially available tile adhesives. The cement industry is, however, increasing its production of CEM II and other types of low-emission cements that have a lower carbon footprint. As CEM I will at some point be taken off the market, tile adhesive manufacturers face the task of replacing Portland cement in their formulations with CEM II or, if necessary, other types of cements. In view of this development, however, an important question needs to be asked as to whether and to what extent the properties of tile adhesives change if CEM I is replaced by CEM II.

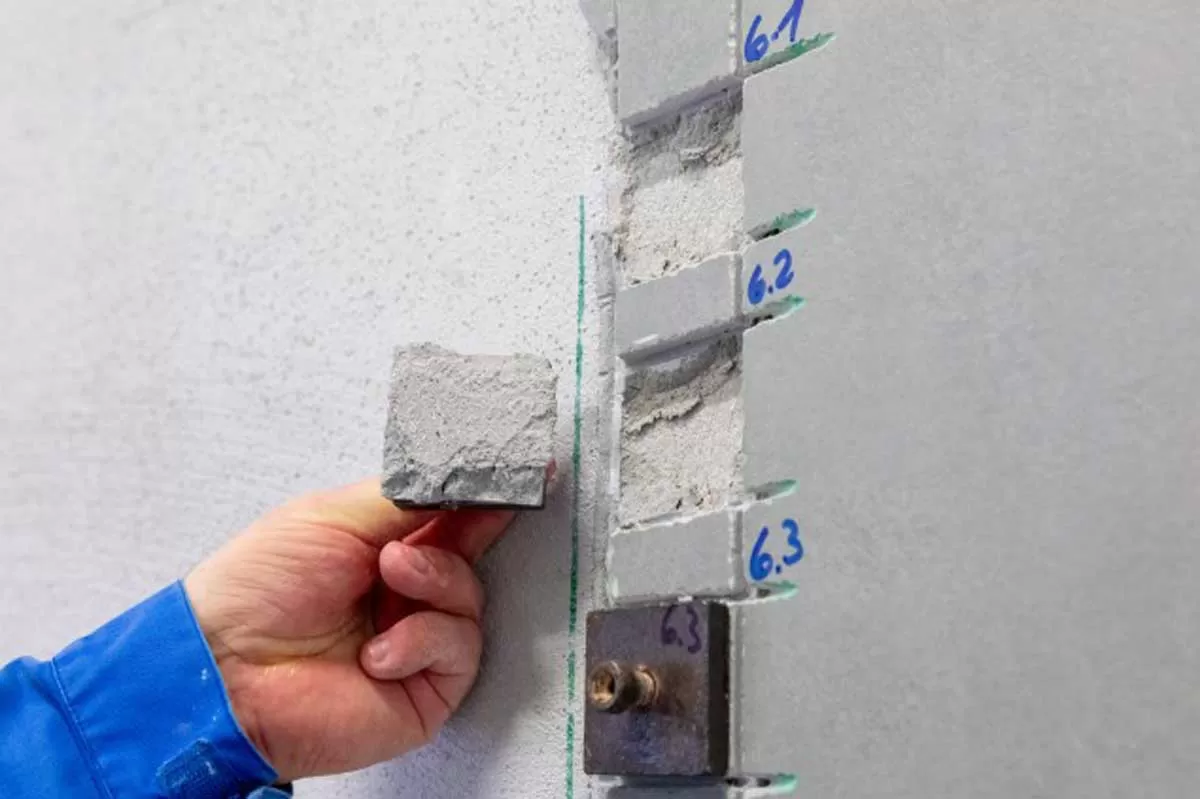
Substituting CEM I with CEM II in tile adhesives WACKER has investigated the extent to which the substitution of CEM I with CEM II will impact the properties of tile adhesives. A tile adhesive classified as C2TE in accordance with European standard EN 12004 (C = cementitious adhesive, 2 = high-strength adhesive, T = high resistance to vertical slip, E = open time of at least 30 minutes) served as a reference sample. In a series of tests, the CEM I content in the reference sample was replaced by four different CEM II formulations. WACKER experts examined if the new formulations are able to fulfill the requirements specified for a C2TE tile adhesive. The test results revealed that most of the properties remained unchanged. As in the case of the reference sample, density and workability, resistance to vertical slip, and wetting capability meet the requirements specified in the standard.

Using CEM II instead of CEM I does, however, have a negative impact on two properties: the tensile adhesion strength following immersion in water and early strength. In contrast to the reference sample, all the CEM II tile adhesive formulations tested had a lower initial tensile adhesion strength and a lower tensile adhesion strength following storage at elevated temperatures and under freeze-thaw conditions. What is crucial, however, is the fact that the tile adhesives formulated with CEM II have such a low tensile adhesion strength following immersion in water that they fail to meet the C2 requirement of 1 N/mm2 as specified in the standard. Tensile adhesion strength of CEM II tile adhesives can be improved by using VINNAPAS© dispersible polymer powders to modify the formulation It is possible to improve the unsatisfactory tensile adhesion strength of CEM II tile adhesives following immersion in water. The key to this is the use of polymer-modified adhesives. Replacing a standard vinyl acetate-ethylene copolymer (VAE) with special terpolymers in which water-repellent monomers are incorporated into the VAE backbone improves the tensile adhesion strength following immersion in water, whereby the requirements specified in the standard are met. In formulations with VINNAPAS® 8118 E, 8620 E or 7220 E, which contain such water-repellent monomers, the tensile adhesion strength following immersion in water is significantly improved and the requirements specified in the standard are thus met.

Conclusion: CEM II cements are suitable as binding agents for tile adhesives. In order to achieve similar performance characteristics as CEM I cements, modifications to the composition of the relevant adhesive are recommended and, in some cases, may even be necessary. To successfully progress in the transition from CEM I to CEM II cements and, at the same time, achieve an improved carbon footprint for tile adhesives, manufacturers of dry-mix mortars can rely on WACKER and its range of VINNAPAS® E grade dispersible polymer powders.

Manufacturers of dry-mix mortars – in particular tile adhesives – are currently facing the challenge of adapting their formulations, which are based on Portland cement (CEM I). Why? With the aim of reducing CO2 emissions, the cement industry is increasingly switching its production to Portland composite cements (CEM II). With a wide range of VINNAPAS® dispersible polymer powders that ensure high-performance formulations of dry-mix mortars, even with CEM II cements, WACKER helps dry-mix mortar manufacturers achieve this transition. At the 2025 European Coatings Show, which will be held in Nuremberg, Germany, from March 25 to 27, WACKER will be presenting a portfolio including polymer dispersions, dispersible polymer powders and solid resins – products that are used in numerous industries to enhance product properties. The cement industry is responsible for around 8% of the world’s total CO2 emissions. Considered a particularly energy and emissions-intensive sector, the cement industry has taken various measures aimed at reducing its CO2 emissions for the benefit of the climate. Some of these measures involve changing the product portfolio to include cements with a lower proportion of Portland clinker. (Portland clinker is the heated part of the cement that is responsible for the setting and hardening of the cement when water is added.) This trend is likely to continue, especially as many industrialized nations have set themselves the goal of producing climate-neutral cement from 2050. In several European countries, among them the Czech Republic, manufacturers have already removed CEM I from their portfolio. In terms of volume, cement, alongside sand, is the most important component of dry-mix mortars and, consequently, tile adhesives. It serves as a binding agent. CEM I is used in many commercially available tile adhesives. The cement industry is, however, increasing its production of CEM II and other types of low-emission cements that have a lower carbon footprint. As CEM I will at some point be taken off the market, tile adhesive manufacturers face the task of replacing Portland cement in their formulations with CEM II or, if necessary, other types of cements. In view of this development, however, an important question needs to be asked as to whether and to what extent the properties of tile adhesives change if CEM I is replaced by CEM II. Substituting CEM I with CEM II in tile adhesives WACKER has investigated the extent to which the substitution of CEM I with CEM II will impact the properties of tile adhesives. A tile adhesive classified as C2TE in accordance with European standard EN 12004 (C = cementitious adhesive, 2 = high-strength adhesive, T = high resistance to vertical slip, E = open time of at least 30 minutes) served as a reference sample. In a series of tests, the CEM I content in the reference sample was replaced by four different CEM II formulations. WACKER experts examined if the new formulations are able to fulfill the requirements specified for a C2TE tile adhesive. The test results revealed that most of the properties remained unchanged. As in the case of the reference sample, density and workability, resistance to vertical slip, and wetting capability meet the requirements specified in the standard. Using CEM II instead of CEM I does, however, have a negative impact on two properties: the tensile adhesion strength following immersion in water and early strength. In contrast to the reference sample, all the CEM II tile adhesive formulations tested had a lower initial tensile adhesion strength and a lower tensile adhesion strength following storage at elevated temperatures and under freeze-thaw conditions. What is crucial, however, is the fact that the tile adhesives formulated with CEM II have such a low tensile adhesion strength following immersion in water that they fail to meet the C2 requirement of 1 N/mm2 as specified in the standard. Tensile adhesion strength of CEM II tile adhesives can be improved by using VINNAPAS© dispersible polymer powders to modify the formulation It is possible to improve the unsatisfactory tensile adhesion strength of CEM II tile adhesives following immersion in water. The key to this is the use of polymer-modified adhesives. Replacing a standard vinyl acetate-ethylene copolymer (VAE) with special terpolymers in which water-repellent monomers are incorporated into the VAE backbone improves the tensile adhesion strength following immersion in water, whereby the requirements specified in the standard are met. In formulations with VINNAPAS® 8118 E, 8620 E or 7220 E, which contain such water-repellent monomers, the tensile adhesion strength following immersion in water is significantly improved and the requirements specified in the standard are thus met. Conclusion: CEM II cements are suitable as binding agents for tile adhesives. In order to achieve similar performance characteristics as CEM I cements, modifications to the composition of the relevant adhesive are recommended and, in some cases, may even be necessary. To successfully progress in the transition from CEM I to CEM II cements and, at the same time, achieve an improved carbon footprint for tile adhesives, manufacturers of dry-mix mortars can rely on WACKER and its range of VINNAPAS® E grade dispersible polymer powders.

Related Stories

Gold Stories

Next Story
Infrastructure Transport

97 Per Cent Of Rongjeng-Mangsang-Adokgre Road Nears Completion

Deputy Chief Minister in-charge of public works Prestone Tynsong said in Shillong on 26 August that 97 per cent physical progress had been achieved on the ongoing Rongjeng-Mangsang-Adokgre road being constructed under the Non-Lapsable Central Pool of Resources (NLCPR). He noted the project was sanctioned in 2017 and that the stipulated time for completion had been 24 months from issue of the final work order. The deputy chief minister informed the assembly that the government had decided to include the remaining work under a World Bank project. In reply to a query from Rongjeng MLA Jim M Sangm..

Next Story
Infrastructure Transport

First TBM Starts Digging Five Point Three Kilometre Tunnel Under SGNP

The Goregaon-Mulund Link Road (GMLR) Phase three (B) project has reached a key milestone as the first tunnel boring machine (TBM) began excavation of the first of two tunnels beneath the Sanjay Gandhi National Park (SGNP). The machine, named Tulsi, started cutting a five point three kilometre bore that will link Dadasaheb Phalke Chitranagari in Goregaon East with Amar Nagar in Mulund West. Officials issued a statement noting the commencement of tunnelling work under the protected green belt. The twin tunnels are being constructed using mechanised tunnelling methods that aim to limit surface di..

Next Story
Infrastructure Transport

UP Approves Two Expressways And Rs 240 bn Infrastructure Push

The Uttar Pradesh Cabinet approved a series of infrastructure and industrial investment proposals totalling Rs 240 billion (Rs 240 bn), including two major expressway projects, a manufacturing and logistics cluster in Sultanpur and incentives for 11 industrial projects across the state. The decisions, taken at a meeting chaired by Chief Minister Yogi Adityanath, underline the state government’s focus on expanding road connectivity around emerging industrial hubs while attracting manufacturing investment to districts beyond major urban centres. The approvals cover both greenfield expressway c..

Advertisement

Subscribe to Our Newsletter

Get daily newsletters around different themes from Construction world.

STAY CONNECTED

Advertisement

SPECIAL OFFER
QR Code