+
Here’s how Bogibeel Bridge was constructed!
ROADS & HIGHWAYS

Here’s how Bogibeel Bridge was constructed!

India recently welcomed one of its biggest landmarks! The country’s longest rail-cum-road bridge—Bogibeel Bridge over river Brahmaputra in Assam—was recently inaugurated, after having encountered several engineering and other challenges, almost 22 years after its foundation stone was laid in January 1997.

For the construction of this mammoth bridge, HCC set-up huge facilities on the left bank of the river for the three sequences of fabrication, assembly and launching.

Fabrication: Fabrication shops of 2,000 mt per month capacity were set up with two parallel bays. The team had assembled customised platforms in house to fabricate and fit various joints employing gas metal arc welding (GMAW). To ensure error-free welding, magnetic particle testing, dry penetration testing and ultrasonic testing were deployed. A specialised beam-making CMM machine from Italy has been used for the first time in India for the fabrication of box and I-sections using the submerged arc welding (SAW) procedure. A blasting gun was used to achieve the surface roughness of SA 2½ before applying paint.

Assembly: Thereafter, these fabricated sections were moved to the assembly shop where they were installed on their designated beds. They were correctly positioned through jacking and welded by GMAW process. These segments were arranged in a sequence and sent for the vertical assembly using horizontal lifters. After installation of the top and bottom girders, the final truss bridge dimension design chambers were examined thoroughly and approved to complete the fitout. A nose was fabricated and fitted on the first truss before launching it on the piers.

Launching: While determining the methodology of erecting the steel trusses on pillars, the engineers had two choices: lift the spans with floating cranes or erect them with a launching truss. They had to choose the more practical and economical option. After weighing the pros and cons, the HCC team came up with the solution of pulling the steel trusses with a set of jacks and winches on the pillars. This eliminated the need to enter the river, which was often turbulent during monsoons. Besides, it also ensured safer working conditions, precluded the mobilisation of a giant set-up on either side of the river having a width of 4.8 km, and accelerated the pace of the project. A 1,000-tonne hydraulic jack and strand jacks linked with the substructures have been used for moving the steel truss over the pillars. Two sets of steel cable strands were anchored to the end cross beams of the truss and hauled by hydraulic jacks. The truss slides over the launching bearing with the help of sliding plates, which were inserted at one end and taken out at the other, thereby moving the truss towards its desired position. To limit the required launching forces, the superstructure was pulled in four launching segments of 10 spans each. Thus, the superstructure was pulled over the pillars just like a train of 10 spans, with each span weighing 1,700 mt. Finally, the launching bearings were replaced by final bearings. The tracks were laid and the road was constructed adapting RCC construction. After fulfilling the electrical and other ancillary requirements, the assignment was completed.

India recently welcomed one of its biggest landmarks! The country’s longest rail-cum-road bridge—Bogibeel Bridge over river Brahmaputra in Assam—was recently inaugurated, after having encountered several engineering and other challenges, almost 22 years after its foundation stone was laid in January 1997. For the construction of this mammoth bridge, HCC set-up huge facilities on the left bank of the river for the three sequences of fabrication, assembly and launching. Fabrication: Fabrication shops of 2,000 mt per month capacity were set up with two parallel bays. The team had assembled customised platforms in house to fabricate and fit various joints employing gas metal arc welding (GMAW). To ensure error-free welding, magnetic particle testing, dry penetration testing and ultrasonic testing were deployed. A specialised beam-making CMM machine from Italy has been used for the first time in India for the fabrication of box and I-sections using the submerged arc welding (SAW) procedure. A blasting gun was used to achieve the surface roughness of SA 2½ before applying paint. Assembly: Thereafter, these fabricated sections were moved to the assembly shop where they were installed on their designated beds. They were correctly positioned through jacking and welded by GMAW process. These segments were arranged in a sequence and sent for the vertical assembly using horizontal lifters. After installation of the top and bottom girders, the final truss bridge dimension design chambers were examined thoroughly and approved to complete the fitout. A nose was fabricated and fitted on the first truss before launching it on the piers. Launching: While determining the methodology of erecting the steel trusses on pillars, the engineers had two choices: lift the spans with floating cranes or erect them with a launching truss. They had to choose the more practical and economical option. After weighing the pros and cons, the HCC team came up with the solution of pulling the steel trusses with a set of jacks and winches on the pillars. This eliminated the need to enter the river, which was often turbulent during monsoons. Besides, it also ensured safer working conditions, precluded the mobilisation of a giant set-up on either side of the river having a width of 4.8 km, and accelerated the pace of the project. A 1,000-tonne hydraulic jack and strand jacks linked with the substructures have been used for moving the steel truss over the pillars. Two sets of steel cable strands were anchored to the end cross beams of the truss and hauled by hydraulic jacks. The truss slides over the launching bearing with the help of sliding plates, which were inserted at one end and taken out at the other, thereby moving the truss towards its desired position. To limit the required launching forces, the superstructure was pulled in four launching segments of 10 spans each. Thus, the superstructure was pulled over the pillars just like a train of 10 spans, with each span weighing 1,700 mt. Finally, the launching bearings were replaced by final bearings. The tracks were laid and the road was constructed adapting RCC construction. After fulfilling the electrical and other ancillary requirements, the assignment was completed.

Related Stories

Gold Stories
Next Story
Infrastructure Urban

KONE Opens India's First Digital Experience Centre in Pune

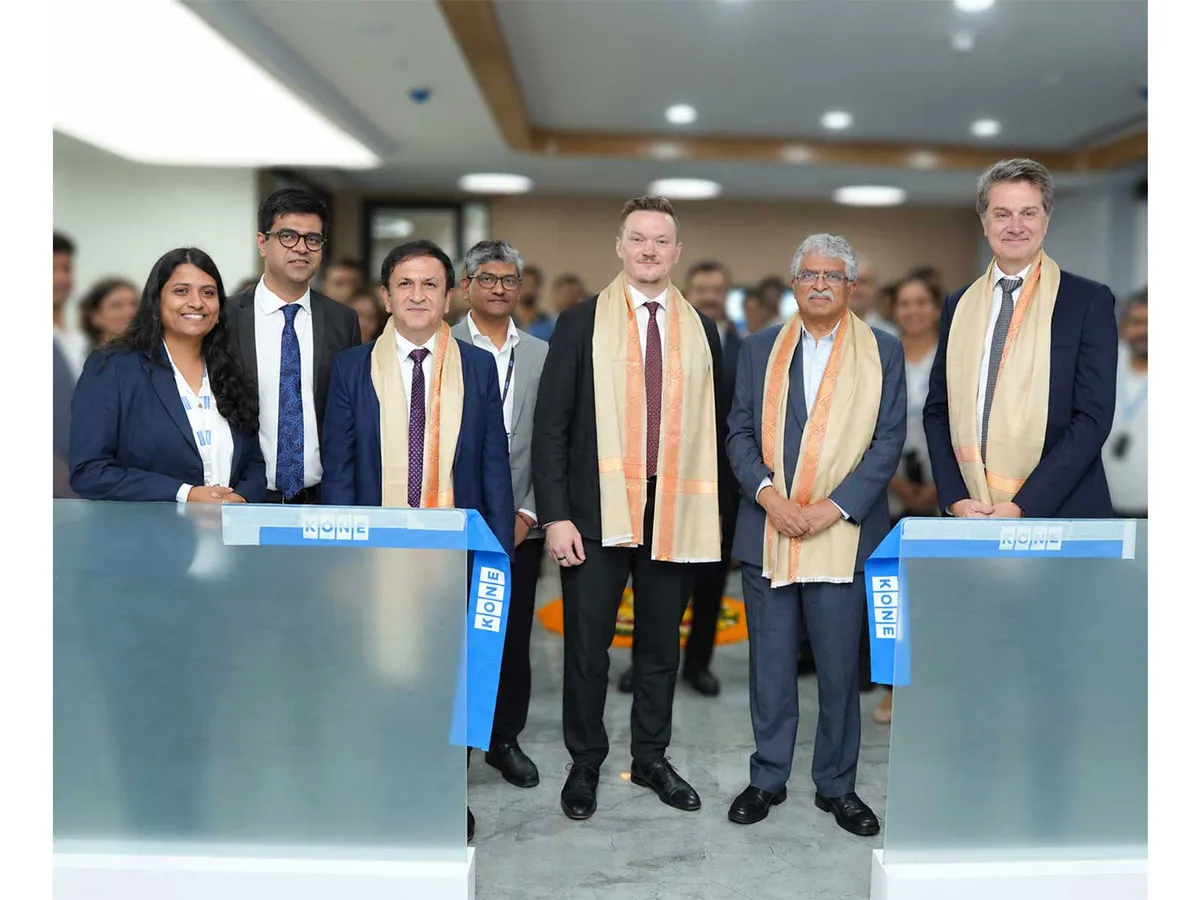
KONE, a global elevator and escalator manufacturer, has inaugurated its first Digital Experience Centre (DEC) in India, located in Pune. The facility aims to showcase how artificial intelligence (AI), connectivity and data-driven technologies can enhance customer experiences and improve building operations.The centre was inaugurated by Jussi Herlin, Executive Vice Chair, KONE Corporation; Philippe Delorme, President and CEO, KONE; and Nandan Nilekani, Co-founder and Chairman of the Board, Infosys.Designed as an interactive customer environment, the facility demonstrates digital solutions cover..
Next Story
Infrastructure Urban

CII GreenCo Launches Circularity Guidelines for Indian Industry

The Confederation of Indian Industry (CII) GreenCo Council has launched the CII GreenCo Circularity Guidelines – Pilot Version at the 17th CII GreenCo Waste & Resource Management Summit 2026 in Chennai. The initiative aims to strengthen resource efficiency, waste reduction and circular economy practices across Indian manufacturing and process industries.The guidelines introduce a structured framework with circularity indices covering raw materials, consumables, packaging and other resource inputs. These indicators will help industries assess existing practices, identify opportunities to ..
Next Story
Infrastructure Energy

Global Electronics Association Launches IPC-1783-CO2E Standard

The Global Electronics Association has introduced IPC-1783-CO2E, a new international standard aimed at improving consistency, transparency and comparability in product carbon footprint reporting across the electronics manufacturing industry.The standard, titled International Standard for Data Collection and Reporting of CO2 Equivalent (CO2e) Emissions for the Electronics Manufacturing Supply Chain, provides industry-specific guidance for collecting, estimating and reporting carbon emissions data.With increasing regulatory requirements and customer expectations, electronics manufacturers face c..

Advertisement

Subscribe to Our Newsletter

Get daily newsletters around different themes from Construction world.

STAY CONNECTED

Advertisement

SPECIAL OFFER
QR Code